

A Powder Metallurgy part can be a cost breakthrough—or an expensive tooling lesson—depending on how early design-for-manufacturing decisions are made. For engineers moving from machining, casting, or MIM, the opportunity is significant: near-net-shape production can deliver high material utilization, stable repeatability, and lower per-part cost at scale. But P/M is not simply a cheaper way to copy a CNC component. Geometry, density, strength, tolerances, and annual volume all affect whether the process will succeed commercially. This guide explains how to define requirements, compare manufacturing routes, and apply practical DFM rules that reduce tooling risk while improving long-term part economics.
Design Goals for Custom Powder Metallurgy Parts
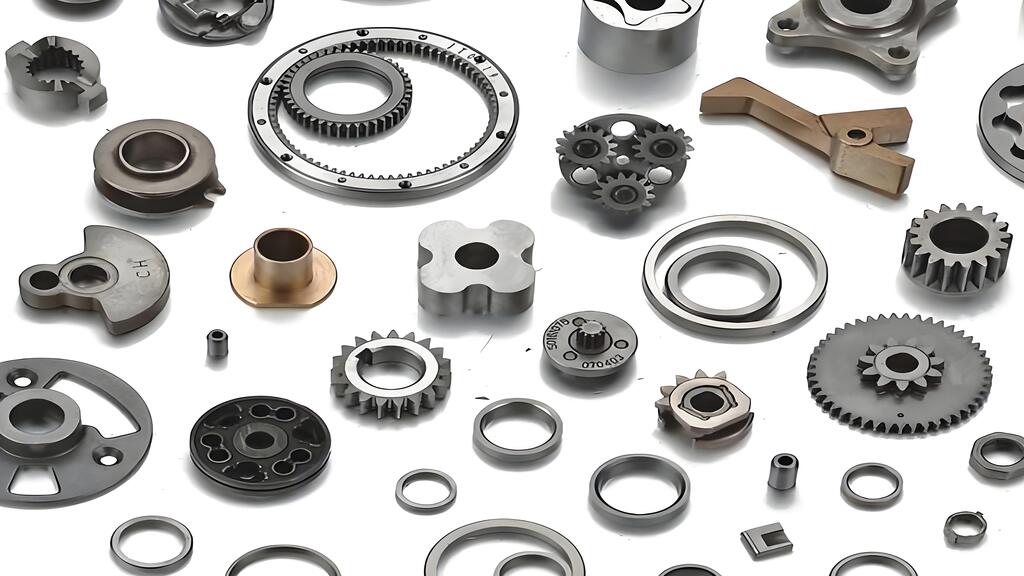
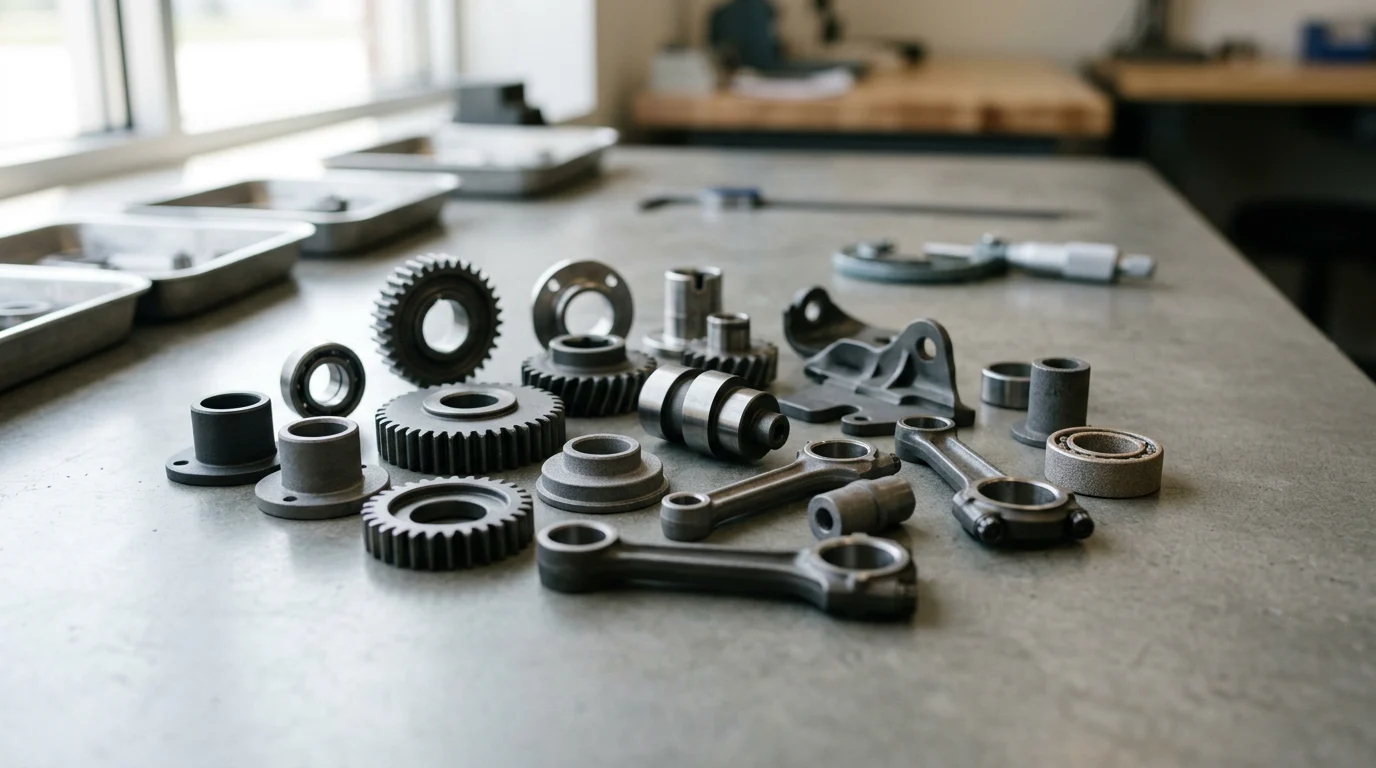
Powder metallurgy(P/M) is a highly efficient process for producing near-net-shape metal components with exceptional material utilization. Shifting from traditional subtractive machining to net-shape processes like P/M offers a distinct competitive advantage for optimizing performance and budgets. A successful transition relies on understanding the fundamental mechanics of powder compaction and Sintering, ensuring the component is designed specifically for the process rather than merely adapted from a machined prototype. Establishing these targets early prevents extensive redesign loops and sets a clear baseline for supplier negotiations.
Define performance and commercial requirements
Baseline material selection and compaction strategy depend directly on application requirements. Engineers must specify expected tensile strength, yield thresholds, apparent hardness, and fatigue limits based on operational stresses. Environmental factors, such as corrosion resistance, dictate whether a standard low-alloy steel or a more expensive 300-series stainless steel powder is necessary.
Commercially, high-precision compaction dies and punches require significant upfront capital, making P/M economically viable at minimum order quantities (MOQs) typically ranging from 15,000 to 50,000 units annually. These figures vary significantly by supplier geography, capability, and part size. Below this threshold, the amortization of tooling costs generally negates the per-part savings achieved through high-speed pressing and minimal material waste.
Compare powder metallurgy with alternative processes
While CNC machining offers superior dimensional precision and allows for complex cross-holes, it generates substantial material waste and scales poorly for high-volume production. Conversely, metal injection molding (MIM) accommodates extreme geometric complexity akin to plastic injection molding but incurs higher feedstock and processing costs. Die casting is highly efficient for non-ferrous metals like aluminum and zinc but cannot process high-strength steel alloys.
Although P/M is often associated with 2D profiles due to vertical compaction limits, it can achieve limited 3D features through multi-level tooling. Secondary machining is commonly utilized for transverse holes, ensuring the process retains valuable geometric flexibility.
| Process | Typical Economic Crossover (Units/Yr) | Material Utilization | Typical Tolerance (As-processed) | Complexity Capability |
|---|---|---|---|---|
| Powder Metallurgy | > 15,000 | > 95% | IT8 - IT9 | Moderate (2.5D / multi-level) |
| CNC Machining | < 10,000 | 40% - 60% | IT6 - IT7 | High (3D profiles) |
| Metal Injection Molding | > 20,000 | > 95% | IT8 - IT10 | Very High (3D profiles) |
| Die Casting | > 30,000 | > 90% | IT9 - IT11 | High (Thin walls) |
Note: Economic crossover volumes are approximate and highly sensitive to part geometry, material selection, and regional labor rates rather than fixed thresholds.
Powder Metallurgy DFM Rules That Reduce Tooling Risk
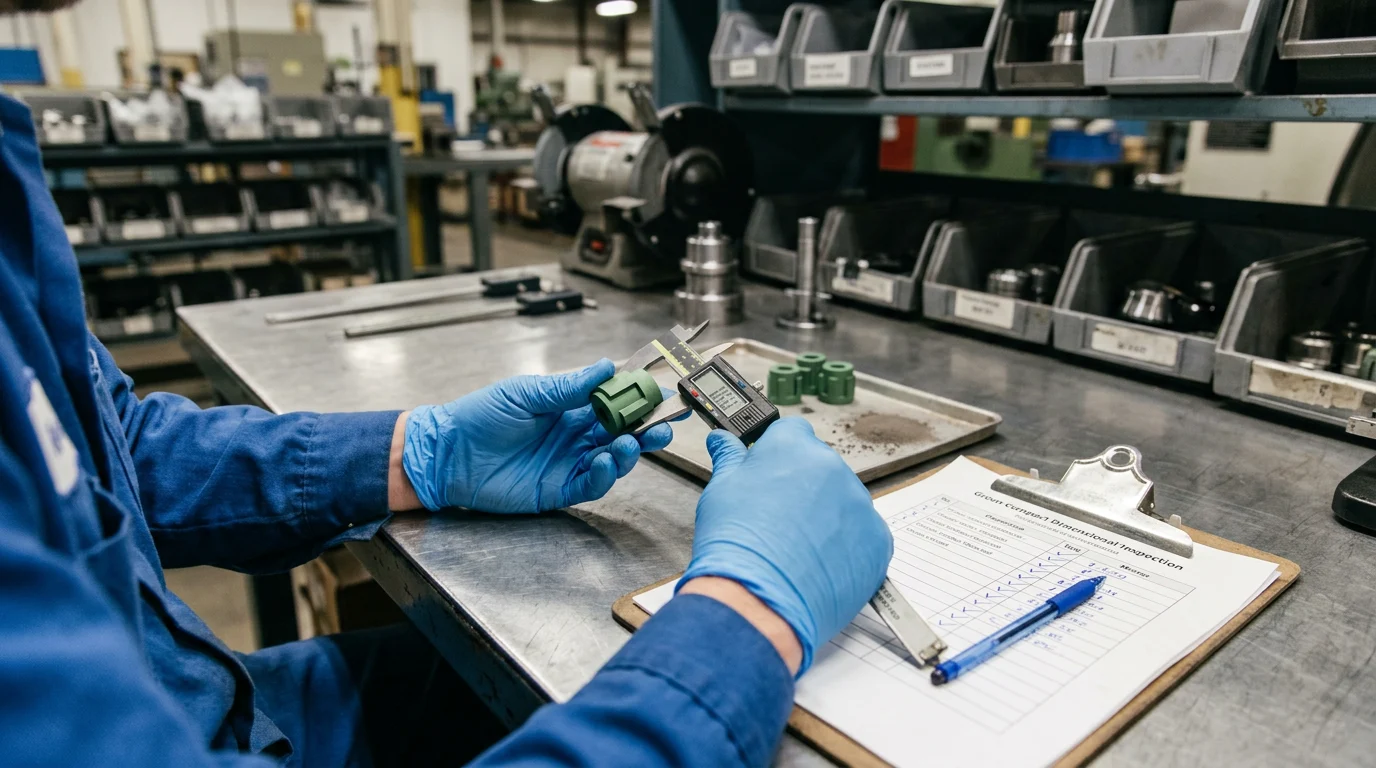
The uniaxial nature of powder compaction inherently restricts certain geometries, demanding proactive design adaptations before committing to hard tooling. Engineers must tailor their CAD models to the realities of rigid dies and vertical press motions to mitigate tooling risks, minimize tool wear, and ensure consistent part ejection. Ignoring these constraints often leads to punch breakage, uneven density distribution, or excessive secondary machining that erodes the economic benefits of the P/M process.
Optimize geometry, density, tolerances, and materials
Geometry and ejection: Undercuts and reverse tapers prevent vertical ejection from the die cavity and must be avoided. While limited transverse holes can sometimes be formed using core rods or split tooling, they significantly increase complexity; otherwise, they must be machined post-sintering. Engineers should maintain a minimum wall thickness of 1.5 mm to prevent punch breakage and ensure uniform powder fill. Sharp corners should be replaced with radii or chamfers to reduce stress concentrations in the tooling. Unlike casting or injection molding, conventional rigid-die axial pressing ejects parts via vertical punches through straight-walled cavities. Therefore, the "no draft angle" rule applies specifically to this rigid-die process—distinguishing it from MIM or isostatic pressing where draft or different geometric constraints may apply—and adding draft can actually introduce harmful density gradients. Designers must also avoid large variations in wall thickness and asymmetric geometries to prevent distortion during sintering.
Density and porosity: Typical as-sintered densities range from 6.4 to 7.2 g/cm³ for ferrous alloys. This range is driven by variables such as the use of base iron versus pre-alloyed powder and the applied compaction pressure, meaning engineers must target a realistic value based on these inputs rather than treating the entire span as equally applicable. Inherent residual porosity can degrade fatigue life, limit hermetic sealing, and accelerate corrosion unless secondary operations like resin impregnation are specified. Achieving higher densities for demanding applications often requires warm compaction, high-temperature sintering, double-press/double-sinter (DPDS) techniques, or copper infiltration.
Tolerance strategy: Specifying standard IT8 to IT9 tolerances for as-sintered radial dimensions minimizes the need for secondary sizing or coining operations, keeping production streamlined.
Model cost drivers before approving tooling
Custom P/M tooling sets typically range from $3,000 to $15,000 for very simple, single-level ferrous tools in specific low-cost geographies. However, tooling in North America or Europe often starts significantly higher; engineers must anticipate these regional cost differences early to avoid budget misalignment. Furthermore, multi-level, carbide, or large-part tooling will escalate costs depending on the number of press levels and punch actions required.
Compaction pressure is another critical cost driver. Depending on the target density, many standard iron grades are pressed at 20 to 40 tons per square inch (TSI), while higher-density requirements can push forces to 50 TSI or more. A part with a large projected surface area demands a higher-tonnage press, carrying a higher hourly machine rate. By minimizing the footprint normal to the pressing direction and consolidating multi-level steps into single-level compaction where possible, engineers can reduce the required press tonnage. Piece-part costs are also heavily influenced by powder material costs, sintering furnace throughput efficiency, and scrap economics. Managing these factors directly lowers capital expenditure and extends the operational life of the dies.
Selecting a Manufacturing Partner
Transitioning from a finalized design to high-volume production requires a manufacturing partner capable of executing rigorous DFM protocols.
Key Takeaways
- Evaluate powder metallurgy early when annual demand is likely above 15,000 units, because tooling amortization is a major factor in total part cost.
- Design the part for vertical powder compaction rather than converting a CNC model directly, as uniaxial pressing limits undercuts, cross-holes, and some 3D features.
- Use P/M to reduce material waste, since near-net-shape production can achieve more than 95% material utilization compared with roughly 40% to 60% for many machined parts.
- Define tensile strength, yield strength, hardness, fatigue, and corrosion requirements before selecting powder materials or density targets.
- Plan secondary operations only where they add value, such as machining transverse holes or achieving tolerances tighter than typical IT8 to IT9 as-processed capability.
- Compare P/M against CNC machining, MIM, and die casting using volume, material, tolerance, and geometry—not unit price alone.
Frequently Asked Questions
When is powder metallurgy more cost-effective than CNC machining?
Powder metallurgy is typically more economical for annual volumes above about 15,000 units, especially when the part can be pressed near-net-shape. CNC is often better for low volumes, prototypes, or highly complex 3D features.
What makes a part a good candidate for custom P/M production?
Good P/M candidates have repeatable high-volume demand, moderate 2.5D geometry, acceptable as-sintered tolerances, and materials that benefit from high utilization. Parts redesigned for vertical compaction usually perform better than machined designs converted directly.
What material utilization can engineers expect from powder metallurgy?
P/M commonly achieves more than 95% material utilization because parts are compacted close to final shape. This helps reduce scrap cost compared with CNC machining, where material utilization may fall around 40% to 60%.
Can powder metallurgy produce holes and complex features?
P/M can produce many axial features and limited multi-level geometries through tooling. Transverse holes, undercuts, and certain 3D features often require secondary machining, so they should be identified early in the DFM review.
What tolerances are typical for as-processed P/M parts?
As-processed powder metallurgy parts commonly fall around IT8 to IT9, depending on material, geometry, density, and sintering control. Tighter tolerances may require sizing, calibration, machining, or other secondary operations.